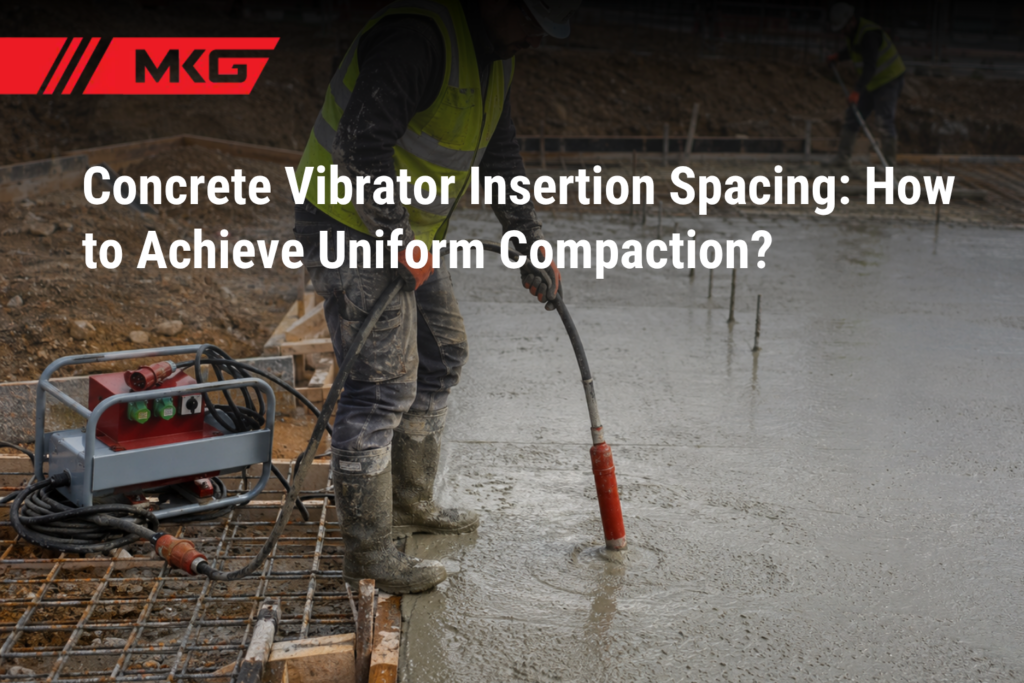
Pour day always looks the same. The mix arrives, the needle goes in, the surface flattens out, and everybody agrees it went well. The truth only shows up two weeks later, when the shuttering comes off and there it is – a patch of exposed stone near the column base, a rough band along the beam soffit, a hollow sound when you tap the wall.
Almost every time, the reason isn’t the mix design. It’s spacing. Somebody put the needle in wherever there was room instead of putting it in at a planned distance and the concrete between two insertion points never got properly worked.
At MKG, we’ve been building light construction machinery in Raipur for years and our needle vibrators go out to sites in every corner of India – tight urban plots, highway stretches, industrial sheds. What we’ve learned from all of it is simple: compaction is not about the machine working hard. It’s about where you put it, and how far apart.
This guide breaks the whole thing down in plain language – the spacing numbers, how to arrive at them for your needle, and the small habits that decide whether your slab is uniformly dense or quietly full of voids.
What "Uniform Compaction" Actually Means
When fresh concrete lands in the formwork, it comes with a lot of trapped air – often 5% to 20% of its volume, depending on how stiff the mix is. That air is not a cosmetic problem. It’s a strength problem.
The widely used field rule is that every 1% of trapped air costs you roughly 5–6% of compressive strength. So a pocket of concrete carrying 5% voids is delivering about a quarter less strength than the cube result on your test report suggested. And because voids also let water and chlorides travel inward, the rebar inside starts corroding much earlier than it should.
“Uniform” is the key word. If half your slab is beautifully compacted and one strip between two insertion points is not, the structure doesn’t average it out. It behaves like the weakest zone. That’s why spacing beats effort every single time.
The Number Everything Depends On: Radius of Action
Picture the needle sitting in wet concrete. Around it, for a certain distance, the concrete briefly turns almost liquid – air rises, particles settle in tighter, mortar fills the gaps. Beyond that distance, nothing meaningful happens.
That circle is called the radius of action (some call it radius of influence). It’s the single most useful thing to understand about vibrator spacing, because it decides everything else.
Two things set its size:
- Head diameter. The bigger the needle, the more concrete it puts into motion and the wider the circle. This relationship is close to direct, which is why needle size is the first spec you should look at.
- Vibration intensity. Frequency and amplitude together decide how hard the needle pushes. A needle running at reduced rpm because of a weak power supply has a smaller circle than the same needle running properly – even though it looks and sounds like it’s working.
Typical radius of action on ordinary structural concrete runs from about 150 mm for a small 25 mm needle up to 400–500 mm for a heavy 60 mm head. Stiffer, lower-slump mixes shrink it. Wetter mixes stretch it.
So How Far Apart Should Each Insertion Be?
Here’s where most sites go wrong: they space insertions at exactly the radius of action, assuming the circles will just touch. In reality, the outer edge of that circle is where vibration is weakest, so two circles touching at the edge leave a badly compacted seam between them.
The whole point of spacing is deliberate overlap. There are two ways to arrive at the number, and they land in roughly the same place.
- Method 1 – The engineering rule. Space insertions at about 1.5 times the radius of action. This is the recommendation in the ACI 309R guide on consolidation of concrete, and the same figure appears in industry practice manuals like the CCAA Guide to Concrete Construction. It guarantees the strong inner zone of one insertion reaches into the strong inner zone of the next.
- Method 2 – The site shortcut. Space insertions at 8 to 10 times the needle diameter, and never more than 600 mm. This is the version worth teaching your operators, because it needs no measurement of anything invisible – just the needle in their hand.
Here’s what that works out to in practice:
Needle diameter | Practical insertion spacing | Where it’s usually used |
25 mm | 200 – 250 mm | Thin slabs, chajjas, narrow columns, congested cages |
40 mm | 320 – 400 mm | General slabs, beams, standard columns |
60 mm | 480 – 600 mm | Rafts, heavy beams, pile caps, mass pours |
75–90 mm | 600 mm (cap it here) | Bridge substructure, large precast elements |
Two adjustments worth remembering. On a stiff, low-slump mix, tighten the spacing by about 20% – the vibration simply doesn’t travel as far. And near formwork faces, keep your insertion line within roughly three-quarters of the radius of action from the shutter, because the face is exactly where honeycombing shows up and exactly where operators tend to under-insert for fear of hitting the ply.
Mark the Grid Before the Truck Arrives
A spacing number that lives only in the site engineer’s head is not a plan. Concrete arrives, the pace picks up, and by the fourth truck the operator is placing the needle by instinct – which drifts wider as the shift wears on, exactly when the pour needs him most.
Set the grid physically instead.
- For slabs, chalk a grid on the shuttering ply before reinforcement goes down, or drop chalk marks on the top mesh once it’s tied. A staggered (triangular) grid covers area more efficiently than a square one at the same spacing, because the circles interlock instead of leaving four-cornered gaps.
- For walls and columns, mark the insertion positions along the top edge of the formwork with a marker or a strip of tape. The operator can’t see below, so a visible mark up top is the only reference he has.
- For long members like beams and retaining walls, work in one direction only. Start at one end and move systematically. Jumping around is how a strip in the middle gets skipped and nobody notices.
Many hoses now carry depth markings every 500 mm, which lets the operator judge insertion depth without guessing. If yours doesn’t, wrap a band of insulation tape at your target depth – it takes thirty seconds and it works.
Pick the Needle That Fits the Cage, Not Just the Member
Spacing assumes the needle actually reaches where it needs to go. In heavily reinforced sections, that’s the real constraint.
As a general guide: 25–40 mm needles suit slabs, chajjas and thin walls; 40–60 mm handles most beams, columns and single-mesh footings; and 60–90 mm is for rafts, heavy footings, girders and precast work. But if the clear gap between bars is 60 mm, a 60 mm needle is not going in cleanly no matter what the member size suggests – it will jam, snag the cage, and end up being dragged sideways.
Where reinforcement is genuinely congested, the fix belongs earlier in the process. Leaving deliberate vibrator access gaps in the cage – typically 100 × 150 mm openings at around 600 mm centres – costs nothing at the detailing stage and saves the pour. That’s a conversation to have while the schedule is still being prepared, alongside your bar cutting and bending planning.
Our needle vibrator range with frequency converter covers the common site diameters so you can match the needle to the cage rather than compromising on either.
Spacing Works in Three Dimensions, Not Two
Your grid handles the plan view. Depth is the other half.
- Keep lifts to 450–500 mm. Deeper than that and the lower portion of the layer sits outside the needle’s effective reach, no matter how long you hold it.
- Push into the layer below by 100–150 mm. This is the step that knits two lifts into one monolithic mass. Skip it and you’ve built a horizontal weak plane straight through your member – the kind of cold joint that shows as a visible line on the finished face.
- Insert vertically and let the needle fall under its own weight. Forcing it in at an angle disturbs the reinforcement and pushes mortar around instead of drawing air up. If it won’t sink, your mix is too stiff for that needle diameter, not the other way around.
How Long to Hold and How to Know When to Stop?
Five to fifteen seconds per insertion covers most structural concrete. Wetter mixes need less, stiffer mixes need more.
But the clock is a backup. The concrete tells you when it’s done, and a good operator reads three signals:
- Air bubbles stop breaking the surface. This is the main one.
- A glossy ring of mortar forms around the needle. The fines have risen and the surface has closed.
- The machine sounds and feels different – the note steadies and the needle runs freer as the surrounding concrete liquefies.
Stopping short leaves honeycombing. Going long causes the opposite problem: segregation. Coarse aggregate settles toward the bottom, mortar and water gather at the top, and you get a weak, dusty surface layer plus extra pressure on the formwork. This is a real risk on high-slump pumped mixes, so if your slump is over 100 mm, be strict about the upper end of the timing.
Withdraw Slowly - the Step Everyone Rushes
Five to fifteen seconds per insertion covers most structural concrete. Wetter mixes need less, stiffer mixes need more.
But the clock is a backup. The concrete tells you when it’s done, and a good operator reads three signals:
- Air bubbles stop breaking the surface. This is the main one.
- A glossy ring of mortar forms around the needle. The fines have risen and the surface has closed.
- The machine sounds and feels different – the note steadies and the needle runs freer as the surrounding concrete liquefies.
Stopping short leaves honeycombing. Going long causes the opposite problem: segregation. Coarse aggregate settles toward the bottom, mortar and water gather at the top, and you get a weak, dusty surface layer plus extra pressure on the formwork. This is a real risk on high-slump pumped mixes, so if your slump is over 100 mm, be strict about the upper end of the timing.
The Mistakes That Quietly Ruin a Good Grid
Five to fifteen seconds per insertion covers most structural concrete. Wetter mixes need less, stiffer mixes need more.
But the clock is a backup. The concrete tells you when it’s done, and a good operator reads three signals:
- Air bubbles stop breaking the surface. This is the main one.
- A glossy ring of mortar forms around the needle. The fines have risen and the surface has closed.
- The machine sounds and feels different – the note steadies and the needle runs freer as the surrounding concrete liquefies.
Stopping short leaves honeycombing. Going long causes the opposite problem: segregation. Coarse aggregate settles toward the bottom, mortar and water gather at the top, and you get a weak, dusty surface layer plus extra pressure on the formwork. This is a real risk on high-slump pumped mixes, so if your slump is over 100 mm, be strict about the upper end of the timing.
Steady Power Is What Makes Spacing Predictable
Here’s a point most articles on this topic skip entirely, and it matters a great deal on Indian sites.
Your entire spacing plan rests on one assumption: that the needle is delivering its rated vibration. But site power rarely cooperates. Long cable runs, shared generator loads, and voltage fluctuations all drag the needle’s rpm down. Frequency drops, amplitude drops, and the radius of action shrinks – silently. The machine still hums, the operator still counts to ten, and the concrete between insertions never gets properly worked.
That’s exactly what a frequency converter is for. It holds the output steady so the needle runs at its designed frequency regardless of what the supply is doing, which means the radius of action you planned around is the radius of action you actually get.
Where mains supply is unreliable or absent, our conventional vibrator range is available in electric and diesel variants and suits thin slabs and wall sections well.
Your Pour-Day Checklist
Before the first truck:
- Needle diameter confirmed against member size and clear bar spacing
- Insertion spacing fixed (8–10 × needle diameter, capped at 600 mm) and marked on ply or formwork
- Lift thickness agreed, no more than 450–500 mm
- Depth marker on the hose
- Standby vibrator on site, converter and cables checked
- Operator briefed on the three stop signals
During the pour:
- Vertical insertions, needle falling under its own weight
- 100–150 mm penetration into the previous lift, every time
- 5–15 seconds, stopping on the visual cue rather than the clock
- Slow withdrawal, roughly 100 mm per second
- Edges, corners and form faces covered by the grid
Why MKG Builds for Indian Pour Conditions?
We design and manufacture in India for the way Indian sites actually run – dust, heat, monsoon interruptions, long shifts, and power that comes and goes. Every machine in our needle vibrator series is built around that reality rather than a catalogue specification.
Good compaction also starts before the needle. Consistent batch-to-batch mixing keeps your radius of action predictable across the pour, which is why our concrete mixers and reversible concrete mixers are built for repeatable output rather than just volume. And once the concrete is in and compacted, timing your finishing correctly protects everything you’ve just achieved – our power trowel timing guide covers that window in detail. If you’re still mapping out which machines your site needs, our guide to building construction equipment and their on-site functions is a useful starting point.
Behind the machines, our spare parts network and rental options exist for a straightforward reason: a vibrator sitting idle during a pour is far more expensive than the vibrator itself.
Compaction isn’t a skill that takes months to learn. It’s a distance, a depth, a count, and a slow lift – repeated honestly across the whole pour.
Need help choosing the right needle size or converter for your next pour?
Talk to our team. Email info@rajat-group.com or call+91 95222 39320 – we’ll help you match the equipment to your section sizes and reinforcement layout.